In PVC pipe production, increasing calcium carbonate loading is a common way to reduce raw material costs per unit of product.
For example, increasing calcium carbonate from 35 phr to 40 phr, 45 phr, or even 50 phr can theoretically reduce the amount of PVC resin required per unit of formulation. However, a lower formulation cost does not necessarily translate into lower overall production costs.
Manufacturers may welcome the savings from higher filler loading while struggling with the processing problems that follow:
-
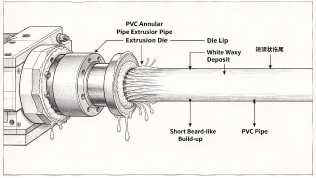
White deposits forming on extrusion dies, die lips, or sizing equipment.
-
More frequent die cleaning, disrupting continuous production.
-
Fluctuations in pipe surface quality, including roughness and uneven gloss.
-
Changes in extrusion load, fusion behavior, or lubrication balance.
-
Repeated adjustments to lubricant dosages in an attempt to resolve processing issues, making the formulation increasingly complex.
Among these issues, white die deposits, also known as die build-up, deserve particular attention.
However, white deposits are not necessarily caused by lubricant exudation, and their chemical composition cannot be determined by appearance alone. To solve the problem effectively, the first step is to identify the source of the deposits and then determine how they relate to the filler system, lubrication system, and processing conditions.
1. Why Can Higher Calcium Carbonate Loading Increase Die Build-Up in PVC Pipe Production?
The key issue is not that more calcium carbonate inevitably leads to more deposits. Rather, changes in filler loading can disturb the processing balance of the original formulation.
1.1. Changes in Filler Content May Make the Existing Lubrication System Less Suitable
PVC extrusion formulations typically contain PVC resin, calcium carbonate, stabilizers, internal and external lubricants, and other processing additives.
These components do not work independently. Together, they influence fusion, melt flow, friction at metal surfaces, and deposit formation during processing.
When calcium carbonate loading increases, the proportion of solid particles rises. This can change the interactions between the resin and filler, the rheological behavior of the system, and the effective distribution of lubricants.
If the original lubrication system was designed for a lower filler loading, it may no longer provide the same processing performance at a higher loading.
Even without changing the lubricant dosage, the formulation may then experience insufficient fusion, excessive external lubrication, a shift in lubrication balance, or other processing abnormalities.
It is important to note that increasing filler loading does not necessarily cause lubricant exudation. The actual outcome depends on factors such as calcium carbonate surface treatment, particle size and dispersion, PVC resin characteristics, lubricant type and dosage, and extrusion temperature and shear conditions.
1.2. Lubricant Migration and Deposition May Be One Source of White Deposits
In PVC pipe formulations, external lubricants generally help regulate friction between the melt and metal processing surfaces, while internal lubricants primarily influence flow and fusion behavior within the material.
If the type, dosage, or combination of lubricants is unsuitable for the current formulation, some components with limited compatibility may migrate during processing and gradually accumulate on the die or other surfaces.
As production continues, deposits may build up and interfere with normal extrusion.
However, this is only one possible cause.
White die deposits may also contain calcium carbonate particles, stabilizer residues, or other additives. In some cases, they may consist of a mixture of several components. Therefore, it is not appropriate to attribute all white deposits simply to excessive lubricant dosage.
1.3. Why Do Deposits Return So Quickly After Cleaning?
If deposits are removed from the die surface without addressing the formulation or processing conditions responsible for their formation, the problem is likely to recur.
For example:
-
If lubricant migration is the main cause, the lubricant types, dosages, and interactions within the system may need to be reassessed.
-
If the deposits contain significant amounts of calcium carbonate, filler dispersion, surface treatment, and processing conditions should be investigated further.
-
If the deposits are related to fusion behavior or temperature distribution, the extrusion process should also be reviewed.
This is why repeated die cleaning may temporarily restore production but cannot replace a systematic investigation of the underlying cause.
2. What Are White PVC Die Deposits? Identify the Source Before Making Adjustments
One of the most common mistakes when dealing with white die deposits is directly increasing or decreasing a lubricant dosage before the cause has been established.
This approach may temporarily improve one processing indicator, but it can also disrupt the existing lubrication balance and create new problems.
A more effective approach is to gather evidence first and determine the appropriate adjustment based on the findings.
Step 1: Analyze the Composition of the Deposits
Start by examining the deposit color, texture, adhesion location, and rate of formation under different production conditions.
Then select appropriate analytical methods based on the actual situation.
For example, Fourier-transform infrared spectroscopy (FTIR) can identify characteristic functional groups in certain organic components, helping assess whether the deposits may contain specific lubricants or other organic additives.
If inorganic fillers or other inorganic components need to be identified, additional methods such as ash analysis, elemental analysis, or other suitable tests may be required.
It is important to understand that FTIR alone cannot directly confirm the complete composition of every deposit. For complex mixtures, the results should be interpreted alongside raw material information, formulation records, and findings from other analytical methods.
Step 2: Review Formulation Changes and Processing Records
Before adjusting the formulation, review the following information.
| Investigation area |
Key points to check |
| Calcium carbonate |
Loading, particle size, surface treatment, moisture content, and dispersion |
| Lubrication system |
Types and dosages of internal and external lubricants, and their interactions |
| Stabilizer system |
Stabilizer types, dosages, and compatibility with other components |
| Extrusion process |
Temperature settings in each zone, screw speed, extrusion load, and output |
| Deposit formation |
Onset time, formation rate, adhesion location, and cleaning intervals |
| Finished product quality |
Surface condition, dimensional stability, and relevant mechanical properties |
In particular, compare whether the white deposits first appeared after increasing calcium carbonate loading, changing lubricants, adjusting stabilizers, or modifying extrusion conditions.
Comparing production records before and after formulation changes can help narrow down the possible causes more effectively.
Step 3: Verify the Cause Through Controlled Comparative Trials
If the lubrication system is suspected, avoid making large changes to several components at once.
A better approach is to establish a baseline formulation, control other conditions as consistently as possible, and adjust key variables step by step while recording the results of each trial.
For example, compare:
-
Processing performance between the original formulation and the high-filler formulation.
-
Die deposit formation under different lubricant combinations.
-
Fusion, flow, and surface quality under different extrusion conditions.
-
Production stability and finished-product performance across different formulation options.
Only targeted comparative trials can establish which changes actually improve the problem, rather than simply making one production trial appear more successful.
3. How Can the Lubrication System Be Optimized for High-Filler PVC Pipe Formulations?
When testing indicates that die build-up is associated with the compatibility of the lubrication system, the goal is not simply to add more lubricant. The entire system needs to be reassessed.
3.1. Rebalance Internal and External Lubrication
Internal and external lubricants serve different functions, but they also influence one another in an actual formulation.
Excessive external lubrication may interfere with PVC fusion, while insufficient lubrication may increase processing resistance and friction against metal surfaces.
Therefore, when filler loading increases, the ratio of internal to external lubricants and their interactions with other formulation components should be reassessed rather than automatically retaining the original dosages.
3.2. Evaluate Lubricant Compatibility with High-Filler Systems
Different lubricants may vary in compatibility, melting behavior, migration tendency, and performance at processing temperatures.
For high-filler PVC formulations, the key is to determine whether a lubricant can provide stable lubrication under the target processing conditions without adversely affecting fusion, melt strength, pipe surface quality, or production stability.
The appropriate adjustment should be determined by the formulation, deposit analysis, and actual test results. A universal dosage recommendation cannot be made independently of the specific system.
3.3. Don’t Overlook the Influence of Calcium Carbonate Itself
The lubrication system is not the only factor that needs to be investigated.
Calcium carbonate particle size distribution, surface treatment, moisture content, and dispersion can also affect its behavior in a PVC system.
If filler dispersion is poor or interactions between the filler and other formulation components change, adjusting the lubricant alone may not fully resolve the deposit problem.
Therefore, optimizing a high-filler formulation requires considering the interactions among the filler, resin, stabilizers, lubricants, and processing conditions.
4. High-Filler Cost Reduction: Don’t Focus Solely on Raw Material Cost per Ton
Increasing calcium carbonate loading is generally intended to reduce formulation costs. However, if it leads to more die cleaning, downtime, scrap, or quality issues, part of the expected savings may be offset.
When evaluating a high-filler formulation, consider at least the following factors:
-
Formulation cost: Unit consumption and purchase costs of resin, calcium carbonate, and various additives.
-
Production efficiency: Die-cleaning frequency, downtime, output, and equipment operating stability.
-
Quality costs: Scrap, rework, surface defects, and the risk of failing performance requirements.
-
Overall processing performance: Fusion behavior, extrusion load, dimensional stability, and finished-product properties.
Only comparisons under actual production conditions can establish whether increasing filler loading delivers a genuine overall cost advantage.
High filler loading does not automatically mean there will be problems, just as lower filler loading does not guarantee lower production costs.
Effective cost reduction means finding a better balance between formulation costs, processing stability, and product performance while meeting applicable standards and customer requirements.
5. How Does Rallychem Help Investigate Die Build-Up in High-Filler PVC Systems?
For white die deposits in PVC pipe production, Rallychem can work with customers to conduct targeted technical assessments using available formulation information, raw material data, processing conditions, and deposit samples.
Our support can include the following:
1. Deposit Analysis
Based on the sample characteristics and actual requirements, we can help identify appropriate analytical methods to investigate the possible organic or inorganic components in the deposits.
2. Formulation and Lubrication System Evaluation
By reviewing calcium carbonate loading, the existing lubricant combination, and processing conditions, we can help identify potential compatibility issues and determine the direction of subsequent trials.
3. Screening Targeted Solutions
Based on the customer’s actual formulation and performance requirements, we can evaluate lubricant solutions worth testing further rather than simply recommending an increase in the dosage of a particular additive.
4. Laboratory and Production Validation
Through laboratory evaluation and production trials on the customer’s line, we can assess changes in die build-up, extrusion behavior, pipe surface quality, and relevant product properties, then continue optimizing the approach based on the results.
For PVC pipe manufacturers using high filler loadings, the goal is not simply to keep the die clean. It is to establish a solution that balances formulation costs, processing stability, and product quality.
If your PVC pipe production is experiencing recurring white die deposits, changes in processing behavior after increasing calcium carbonate loading, or difficulties balancing the lubrication system,
contact the Rallychem technical team.
Providing basic formulation information, deposit samples, and processing conditions can help us investigate the problem more effectively and discuss optimization options suited to your production system.






 English
 Español
 Français
 日本語
 한국어
 العربية
 فارسی
 Deutsch
 Italiano
 Tiếng Việt
 ไทย
 Русский
 Bahasa Indonesia
 Bahasa Melayu
 Türkçe


